

Industrial Water Softening Without Salt: Alternatives and Performance
Industrial facilities increasingly need to manage hard water without adding sodium chloride to a regeneration cycle. High hardness can create scale in boilers, heat exchangers, cooling systems, membranes, washing equipment, and process lines. The resulting loss of heat transfer and unplanned maintenance can be more expensive than the original water-treatment system.
Salt-free water conditioning offers a different operating model. Instead of exchanging calcium and magnesium for sodium, many alternatives prevent minerals from forming firmly attached deposits, while others physically separate hardness from the water. The right choice depends on whether a facility needs genuine hardness removal, scale prevention, lower discharge volumes, or a combination of these outcomes.
Industrial water softening without salt is therefore not one technology. It is a group of treatment approaches with different capabilities, limits, energy requirements, and maintenance profiles. Performance should be assessed against the process target rather than against a generic promise of “soft water.”
What hard water does to industrial systems
Hardness mainly comes from dissolved calcium and magnesium. When heated, concentrated, or exposed to changing pressure, these minerals can combine with carbonate, sulfate, or silica and form deposits. Calcium carbonate is common in hot-water circuits, while calcium sulfate and mixed mineral scale can become serious concerns in evaporative or high-recovery systems.
Scale reduces the effective diameter of pipes and increases pumping resistance. On heat-transfer surfaces, even a thin mineral layer acts as insulation, forcing boilers, pasteurizers, chillers, and heat exchangers to consume more energy. Hard water can also interfere with detergents, rinsing, textile processing, food production, and industrial washing.
A water analysis should measure total hardness as calcium carbonate, calcium and magnesium separately, alkalinity, pH, conductivity, silica, sulfate, chloride, iron, manganese, and temperature. These values reveal whether the main issue is hardness, a broader mineral balance, or another contaminant that could be mistaken for a softening problem.
Salt-free technologies and how they work
Template-assisted crystallization, often marketed as a salt-free scale-control process, uses a catalytic media surface to encourage dissolved minerals to form microscopic crystals. The crystals remain suspended and pass out with the water instead of attaching strongly to equipment. This approach can reduce scale formation while preserving calcium and magnesium in the treated water.
The key distinction is that crystallization media generally condition hardness rather than remove it. Conductivity and total dissolved solids may remain almost unchanged. This makes the method attractive for cooling water, commercial hot-water systems, and selected process applications where mineral removal is unnecessary but deposit control is the priority.
Nanofiltration can remove a substantial portion of divalent ions, including calcium and magnesium, while allowing some monovalent salts to pass. Reverse osmosis removes a wider range of dissolved minerals and can produce low-hardness water for boilers, manufacturing, rinsing, and high-purity applications. Both membrane processes require pretreatment and generate a concentrate stream that must be managed.
Electrochemical systems, capacitive deionization, and specialized adsorption media may also reduce hardness in defined operating conditions. Their suitability depends on feedwater chemistry, flow rate, regeneration or electrode cleaning requirements, and the acceptable quality of the treated water. They should be evaluated through pilot testing rather than selected solely by equipment category.
Comparing performance in industrial applications
A useful comparison separates scale control from hardness reduction. A facility supplying a cooling loop may need reliable protection against deposits, while a boiler makeup system may require low hardness and low silica. Treating these two duties as identical can lead to inadequate protection or unnecessary capital and operating costs.
| Technology | Main result | Salt use | Waste stream | Typical strengths | Main limitations |
|---|---|---|---|---|---|
| Template-assisted crystallization | Reduces adhesion of mineral scale | None | Usually none beyond normal drain flow | Low maintenance, no brine, retains minerals | Does not substantially lower hardness or TDS |
| Nanofiltration | Removes much of the calcium and magnesium | None | Membrane concentrate | Lower pressure than reverse osmosis, selective hardness reduction | Requires pretreatment and concentrate handling |
| Reverse osmosis | Broad dissolved-solids reduction | None | Concentrate, often significant | Produces low-hardness water for demanding processes | Higher energy, pretreatment, and membrane care |
| Electrodialysis or related electrochemical treatment | Selective ion reduction | None | Concentrate or cleaning waste | Adjustable separation and continuous operation | More complex controls and chemistry sensitivity |
| Conventional ion exchange | Exchanges hardness ions for sodium or hydrogen | Usually regenerant salt | Brine or regeneration waste | Proven, predictable softening performance | Salt handling, wastewater, and sodium increase |
For true soft-water specifications, nanofiltration or reverse osmosis is usually more appropriate than a scale conditioner. For moderate-temperature systems with acceptable dissolved mineral content, catalytic crystallization may offer a simpler alternative. A hybrid arrangement can be effective: membrane treatment for critical makeup water, followed by scale control or polishing for a specific circuit.
Performance should be measured over time. Important indicators include hardness leakage, scaling rate, pressure drop, heat-transfer efficiency, permeate recovery, membrane differential pressure, conductivity, and cleaning frequency. A system that achieves low hardness but requires frequent chemical cleaning may be less sustainable than a lower-energy conditioner that prevents deposits reliably.
Pretreatment determines reliability
Salt-free equipment cannot compensate for poorly characterized feedwater. Suspended solids can foul membranes and obstruct media beds, while iron and manganese may oxidize and create deposits that resemble hardness scale. Organic matter, oil, chlorine, and biological growth can also reduce membrane life or disrupt catalytic surfaces.
Where iron or manganese is present, oxidation and filtration may be needed before hardness control. The oxidation process in chemical-free iron removal explains why dissolved metals must be converted into filterable particles before they reach downstream equipment. This type of pretreatment can protect membranes, heat exchangers, and polishing stages.
Hydrogen sulfide and other reduced compounds may create odor, corrosion, and treatment complications. Catalytic media can support their conversion and removal when correctly matched to the water chemistry; the science behind catalytic filtration is relevant when a hard-water problem exists alongside sulfur odors or reducing conditions.
Pretreatment may include screening, multimedia filtration, activated carbon, aeration, oxidation, cartridge filtration, or ultraviolet disinfection. The design should also account for seasonal changes, well recovery, production schedules, and periods of low flow. Stable feedwater creates more predictable performance and lowers the risk of premature replacement.
Matching the process to the water duty
Boiler makeup requires especially careful design. Low-pressure boilers may tolerate more dissolved material than high-pressure systems, but hardness leakage can still cause rapid scaling. Reverse osmosis followed by appropriate polishing is commonly considered where steam quality, silica control, or strict conductivity limits are important.
Cooling towers present a different challenge. The objective is often to control cycles of concentration and scale while minimizing blowdown. A salt-free crystallization process may help in suitable chemistry, but it does not eliminate the need to manage conductivity, corrosion, biological growth, and concentration of sulfate or silica.
Food and beverage plants, laundries, agricultural operations, and livestock facilities may prioritize water quality, wastewater reduction, or protection of heated equipment. Nanofiltration can reduce hardness with less mineral rejection than reverse osmosis, potentially lowering energy use and concentrate volume. However, membrane selection must consider sanitation, cleaning compatibility, flow interruptions, and local discharge rules.
Swimming pools, buildings, mobile units, and emergency systems may favor compact equipment with limited chemical storage. In these applications, a no-salt conditioner can simplify logistics when the goal is scale protection rather than mineral removal. Industrial users should define the required output quality in measurable terms before choosing a compact or mobile format.
Operating costs and sustainability
The financial comparison should include more than the purchase price. Salt-free systems may avoid bulk salt storage, brine tanks, regeneration wastewater, and deliveries. Membrane systems avoid salt but consume electricity and produce concentrate. Conventional ion exchange often has modest energy demand but can create a substantial brine-management obligation.
Water recovery is a central membrane metric. A system operating at 75% recovery sends approximately one quarter of its feed to concentrate, although the actual figure depends on scaling potential and membrane design. Higher recovery can reduce water loss but may increase the concentration of sparingly soluble minerals and raise cleaning requirements.
A life-cycle assessment should account for pumps, media replacement, membranes, cleaning chemicals, disposal, maintenance labor, downtime, and the energy penalty caused by scale. Reliable monitoring can improve sustainability by preventing both under-treatment and excessive treatment. Conductivity, hardness, flow, pressure, and temperature sensors help operators identify changes before they become production problems.
For independent guidance on water treatment equipment, applications, and treatment technologies, Swiss Cleanwater Group provides technical information relevant to municipal, industrial, agricultural, and mobile water systems.
Practical recommendations for selecting a system
A disciplined selection process reduces the risk of buying a technology that solves the wrong problem.
- Define whether the target is actual calcium and magnesium removal, scale prevention, lower sodium, reduced wastewater, or a combination of these goals.
- Test the source water during representative operating conditions, including hardness, alkalinity, silica, iron, manganese, sulfate, conductivity, pH, and temperature.
- Compare membrane recovery, concentrate disposal, energy use, media life, cleaning frequency, and maintenance labor over the expected service life.
- Pilot the preferred technology on the most sensitive process or heat exchanger before making a plant-wide commitment.
- Install monitoring for hardness leakage, conductivity, pressure drop, flow, and scaling indicators so performance can be verified continuously.
Salt-free water treatment can deliver strong industrial results when its purpose is clearly defined. A crystallization conditioner may be an efficient scale-control solution, while nanofiltration or reverse osmosis is better suited to applications that demand genuinely low-hardness water. Pretreatment, process matching, and long-term measurement ultimately determine whether the system performs as promised.
Contact Swiss Cleanwater Group to discuss source-water analysis, pilot testing, and a treatment configuration designed around your process requirements. A properly selected system can protect equipment, reduce chemical and salt dependence, and maintain dependable water quality without adding unnecessary waste.
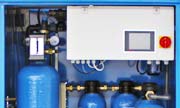
SCM 24
|
|
Cleans 24.000 liters per day
|
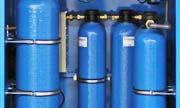
SCM 60
|
|
Cleans 60.000 liters per day
|
Video: How it works
The SCG Advantage
Our market-leading, water cleaning solutions have many advantages. To read more click the items below:
No Chemicals
Our machines and technology does not use any chemicals, at all.
Read more...
No Waste Water
Our machines do not waste any water. Yield = 100%.
Read more...
Low energy use
Uses 50 times less energy than a Reverse Osmosis Machine.
Read more...
Low ownership cost
Lower maintenance and operation costs due to our technology.
Read more...
Easy to install
Simple "plug and play" installation makes for easy deployment.
Read more...
Extremely compact
A compact system, contained in an easy to transport cabinet.
Read more...
Outperforms R.O.
SCG technologies outperform Reverse Osmosis systems.
Read more...
Faster ROI
Get a faster Return on Investment with our systems.
Read more...
Latest News
Latest Blog Posts
| Chemicals in water treatment? |
| Water storage - Whats best for keeping water clean and drinkable? |
| Case: Disaster Management Water Treatment |
Contact SCG
891 Showroom Place
Suite 101
Chula Vista, CA, 91914
Phone: +1 619-878-2730
Contact us by email